PET bottle making
PET blow moulding machines, matched to your bottle and output.
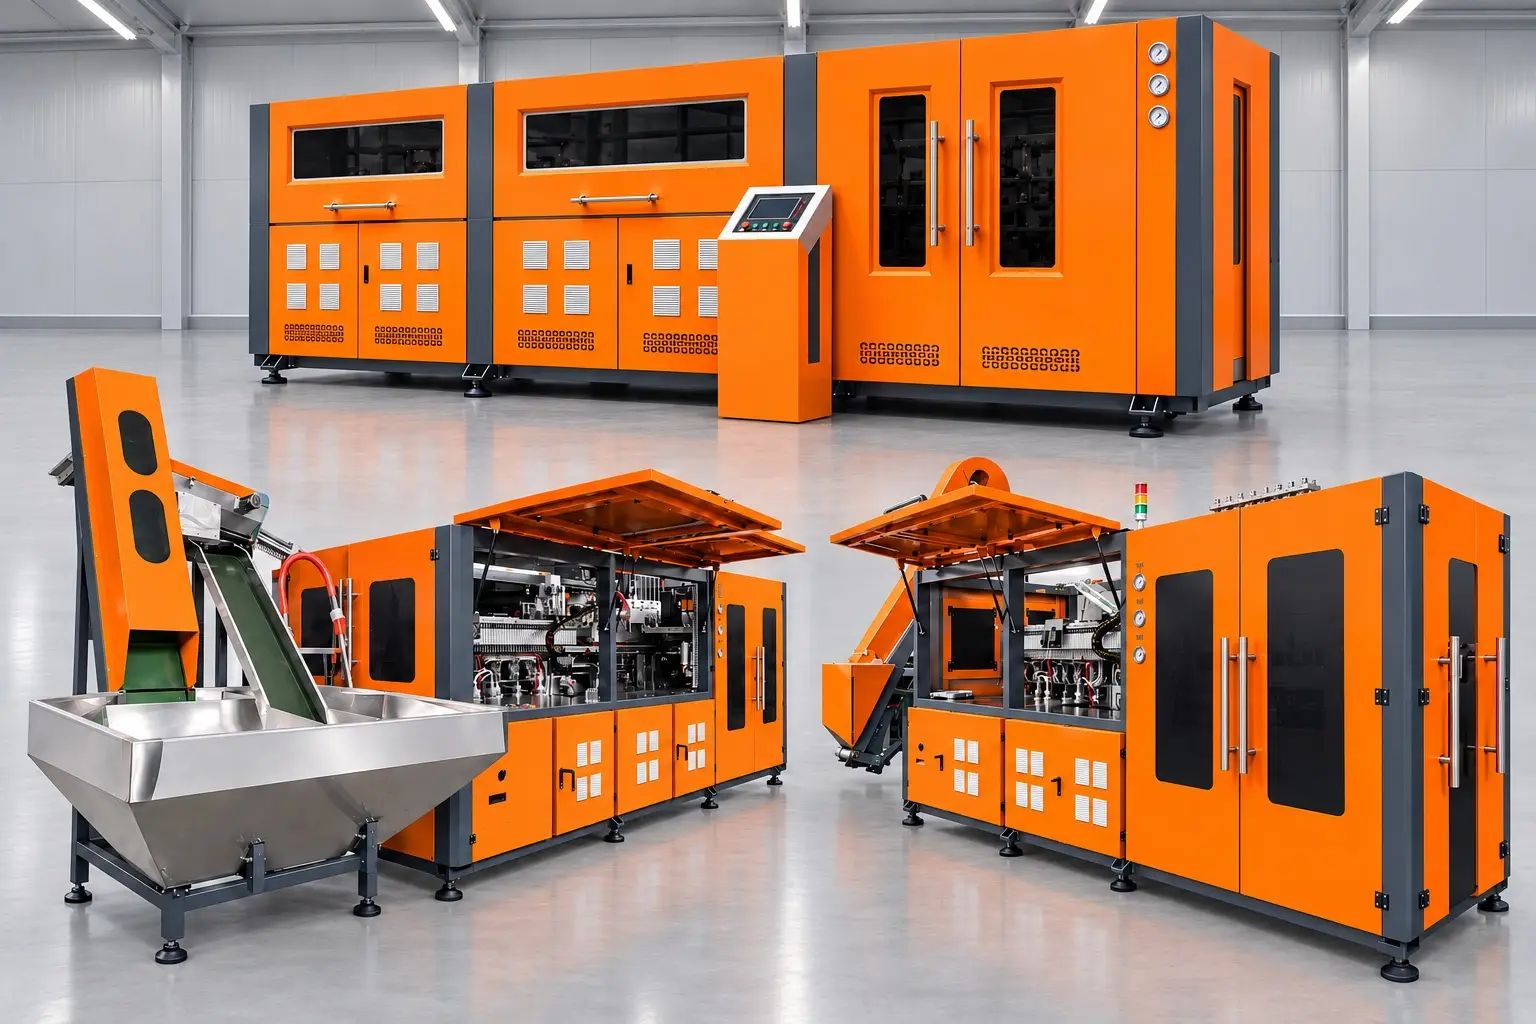
We build semi-automatic and hand-feed PET stretch blow moulding machines for bottles from 30 ml and jars up to 25 L. For bottle production linked to the filling line, we supply and integrate fully automatic machines with theoretical outputs from 2,200 to 12,000 BPH.
Our core focus
Semi-automatic and hand-feed PET stretch blow moulding.
We build the blowing machine with compatible preform heating, moulds and controls. The machine, moulds and auxiliary equipment are selected for your preform, bottle geometry, neck finish and required output.
Production setup
Main equipment Built by ARV
- Main blowing machine
- Preform heating system
- Pneumatic controls
- PET bottle moulds
Auxiliary equipment
- Air compressor
- Air preparation system
- Refrigerated air dryer
- Water chiller
Auxiliary and utility equipment is selected and coordinated with the blowing machine. Model output and the operating arrangement are defined in the technical offer.
Straightforward semi-automatic operation
Preforms are loaded by hand, with a separate heating system and blowing machine. Suitable for small and medium bottled-water and beverage operations.
Customised to your bottle and output
Bottle size, neck finish, moulds, required output and auxiliary equipment are selected around your project. See the ARV-PB model specifications.
Bottle production as a complete setup
The air compressor, air-treatment equipment, dryer, chiller, moulds and electrical load must be coordinated with the blowing machine. Bottles and large jars use separately selected models.
Match blowing output to filling demand
Required bottle supply, operating hours and buffer arrangements determine the machine choice. For online bottle supply to the filling line, see the fully automatic online option.
Workshop at Plot No. 08, Sikandrabad. Facilities are being developed. They are planned to include machining of PET blowing-machine parts, with lathe, milling and VMC equipment.
ARV-PB series
Semi-automatic models, from 30 ml bottles to 25 L jars.
An indicative model range for bottles and jars. Final specifications are confirmed with the quotation.
| Specification | ARV-PB-2AD | ARV-PB-4B | ARV-PB-T2 | ARV-PB-2BJ | ARV-PB-20J |
|---|---|---|---|---|---|
| Application | Auto-Drop | 4-Cavity | Twin Series | Bottle / Jar | 20 L Jar |
| Product range | 30–1,000 ml | 30–1,000 ml | 50–1,000 ml | 50–3,000 ml | 10–25 L |
| Mould cavities | 2 | 4 | 2 (as listed) | 2 | 1 |
| Production output | 900–1,100 BPH | 1,400–1,600 BPH | 2,500–3,000 BPH | 700 BPH / 450 JPH | 90–160 units/hr |
| Neck diameter | 19–30 mm | 19–30 mm | 19–28 mm | 19–30 mm | 52–135 mm |
| Heater power | 10.5 kW | 13.5 kW | 15 kW | 7.5 kW | 18 kW |
| Operating pressure (kgf/cm²) | 6–8 | 6–8 | 6–8 | 6–8 | 6–10 |
| Blowing pressure (kgf/cm²) | 22–25 | 22–25 | 25–30 | 22–25 | 25–30 |
| Air consumption (CFM) | 35.3 | 35.3 | 42.4 | 28.3* | 56.5* |
| Clamping stroke | 150 mm | 150 mm | 150 mm | 200 mm | 350 mm |
| Machine area | 2 × 3.5 m | 2 × 3.5 m | 2 × 3.5 m | 2 × 3.5 m | 4 × 4 m |
| Heater type | IR rotary | IR rotary | IR rotary | IR rotary | IR rotary |
| Operation | Hydro-pneumatic | Hydro-pneumatic | Hydro-pneumatic | Hydro-pneumatic | Hydro-pneumatic |
| Staff required | 2 persons | 2 persons | 2 persons | 2 persons | 2 persons |
| Utility area | 3 × 5 m | 3 × 5 m | 3 × 5 m | 3 × 5 m | 3 × 5 m |
Model key: B = bottle; J = jar; PB = PET blowing; AD = auto drop; T = twin; BPH = bottles per hour; JPH = jars per hour.
*Air consumption for ARV-PB-2BJ and ARV-PB-20J was supplied in M/min and is read here as m³/min; confirmation required. 1 m³/min = 35.315 CFM. FAD and reference conditions are not specified.
Heater power is not the total connected load. Output depends on product size and operating conditions. Technical specifications and data are subject to change without prior notice.
Fully automatic PET series
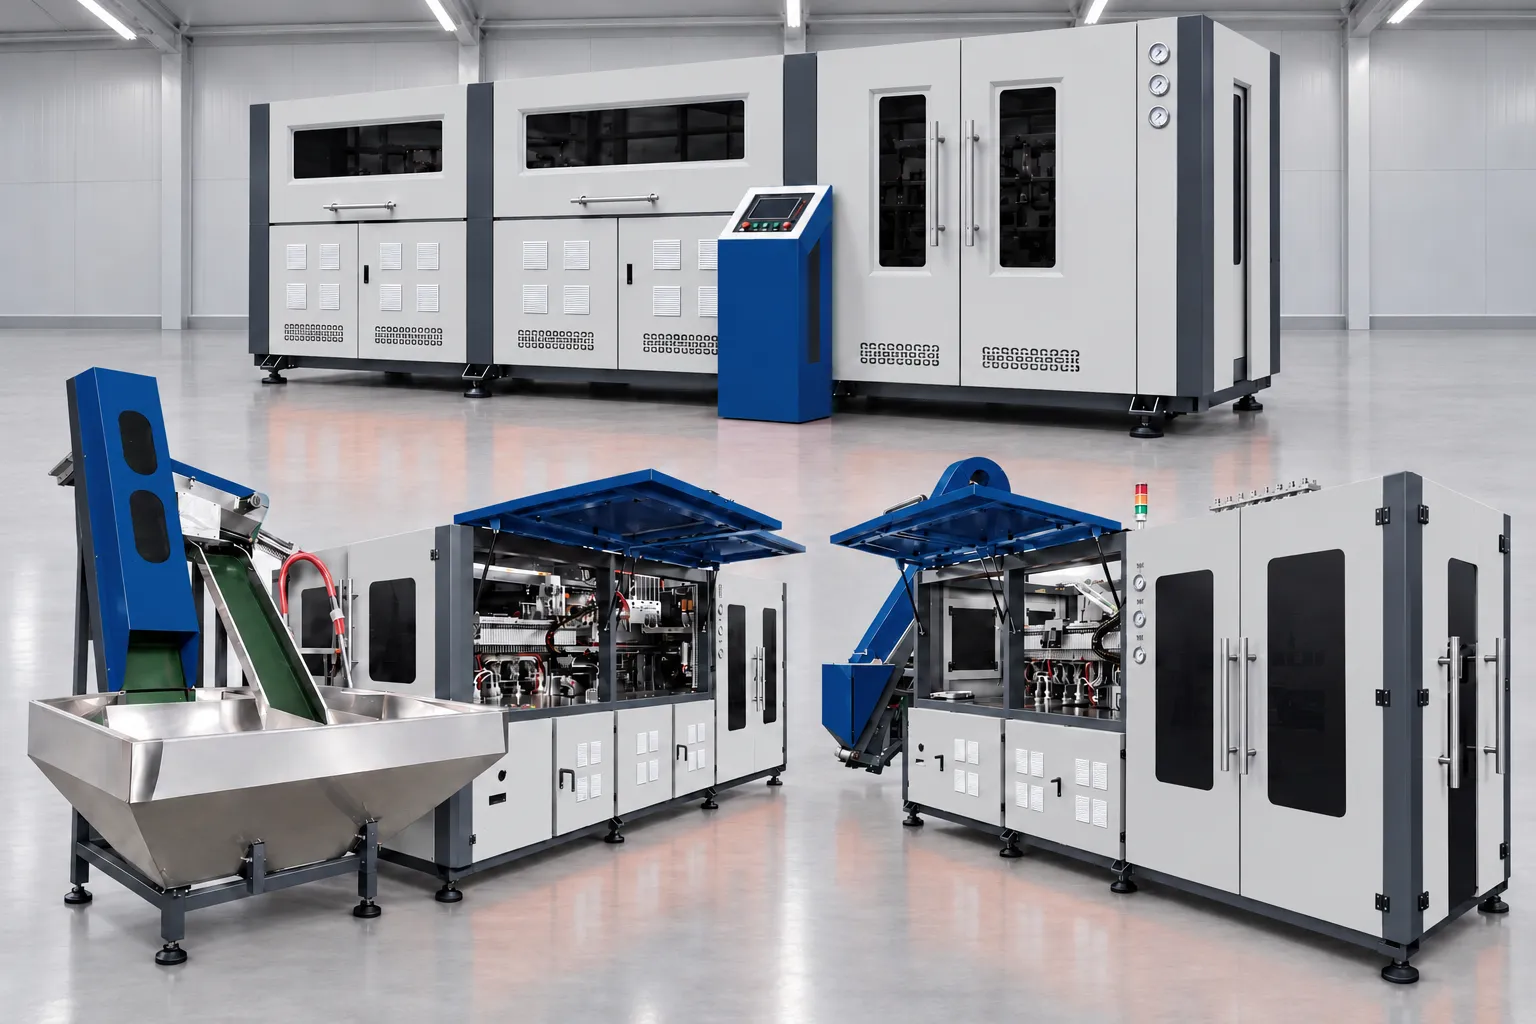
High-speed indexing machines for production from preforms.
Six models with different cavity configurations, bottle-size limits and theoretical outputs. Maximum bottle volume is 600 ml or 2 litres, depending on the model.
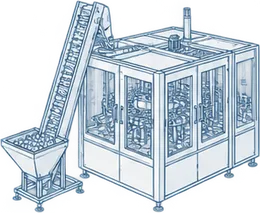
- 2,200–12,000 bottles/hour theoretical output
- 6 models
- 600 ml / 2 L maximum bottle volume, by model
Selected & integratedFully automatic PET blowing machines are selected from Indian and international suppliers and integrated by ARV with your line. Current manufacturing and supply arrangements are defined in the proposal.
In-house bottle production
Produce bottles to your own production schedule.
Bottle supply control
Reduce dependence on empty-bottle suppliers.
Convenient preform storage
Store preforms and blow bottles when required.
Bottle design flexibility
Use compatible moulds and suitable change parts.
Capacity selection
Match bottle size, output and line demand.
Reduced manual handling
Automatic production reduces repetitive handling.
Model range
Fully automatic model range and technical specifications.
The ARV high-speed indexing series. Select the machine around your bottle, preform, utilities and required production output.
| Specification | ARV-2 (2L) | ARV-4 | ARV-4 (2L) | ARV-6 | ARV-6 (2L) | ARV-10 |
|---|---|---|---|---|---|---|
| Maximum bottle volume (L) | 2 | 0.6 | 2 | 0.6 | 2 | 0.6 |
| Theoretical output (BPH) | 2,200 | 6,000 | 5,000 | 9,000 | 8,000 | 12,000 |
| Number of cavities | 2 | 4 | 4 | 6 | 6 | 9* |
| Maximum bottle diameter (mm) | 108 | 72 | 108 | 72 | 108 | 72 |
| Maximum bottle height (mm) | 320 | 260 | 320 | 260 | 320 | 260 |
| Maximum mouth diameter (mm) | 45 | 38 | 38 | 30 | 38 | 30 |
| Maximum preform height (mm) | 180 | 160 | 180 | 160 | 180 | 160 |
| Shifting servo | S | S | S | S | S | S |
| Stretching servo | O | S | S | S | S | S |
| Mould closing servo | O | S | S | S | S | S |
| Preform dividing servo | N/A | N/A | S | S | S | S |
| Heating spacing (mm) | 114.3 | 76.2 | 114.3 | 76.2 | 114.3 | 76.2 |
| Heating zones | 3 | 4 | 4 | 4 | 5 | 8 |
| Number of heating lamps | 24 | 28 | 32 | 28 | 32 | 52 |
| Bottle grippers | 48 | 92 | 76 | 108 | 90 | 180 |
| Movement air (m³/min) | 1.6 | 2 | 2 | 2.5 | 2.5 | 3 |
| Movement pressure (MPa) | 0.8–0.85 | 0.8–0.85 | 0.8–0.85 | 0.8–0.85 | 0.8–0.85 | 0.8–0.85 |
| Blowing air (m³/min) | 1.6 | 3.2 | 4 | 5 | 5 | 8 |
| Blowing pressure (MPa) | 2.5–3.0 | 2.5–3.0 | 2.5–3.0 | 2.5–3.0 | 2.5–3.0 | 2.5–3.0 |
| Operating power (kW) | <20 | <25 | <30 | <36 | <42 | <50 |
| Installed power (kW) | 70 | 96 | 96 | 120 | 140 | 200 |
| Chiller specification (HP) | 5 | 5 | 5 | 10 | 10 | 15 |
| Machine dimensions L × W × H (m) | 2.65 × 1.9 × 1.98 | 3.4 × 1.7 × 1.9 | 3.888 × 2.0 × 1.98 | 4.3 × 1.9 × 1.9 | 5.0 × 2.25 × 1.98 | 6.38 × 2.28 × 1.9 |
| Machine weight (kg) | 2,500 | 4,500 | 4,500 | 6,200 | 6,500 | 8,000 |
*ARV-10: 9 cavities are listed in the supplied chart; confirm before final quotation.
Theoretical output and high-pressure air consumption are based on a 500 ml water bottle. Actual output depends on bottle and preform specifications and operating conditions. Final configuration is confirmed in the approved technical quotation.
Selection guide
Features, applications and performance.
What changes from model to model, and what to check before you choose.
Servo-controlled transfer
The shifting servo is standard on all six models. Servo stretching and mould closing are standard on ARV-4, ARV-4 (2L), ARV-6, ARV-6 (2L) and ARV-10, and optional on ARV-2 (2L).
Preform handling and heating
The preform dividing servo is standard on ARV-4 (2L), ARV-6, ARV-6 (2L) and ARV-10, and not available on ARV-2 (2L) or ARV-4. Heating is model-specific, with 3–8 zones and 24–52 lamps.
Production and utility selection
Cavity configurations and bottle-size limits let you select for your own production needs. Blowing pressure is 2.5–3.0 MPa and movement pressure is 0.8–0.85 MPa across the series.
Applications and bottle compatibility
For compatible PET bottles for packaged drinking water and other products, subject to bottle design, preform specification, neck dimensions and mould selection. Juice, carbonated beverage, edible oil and specialised bottles need confirmation of the right design and machine configuration. Hot-fill suitability needs separate technical approval.
Performance and plant power planning
Rated output in the specification table is for a 500 ml water bottle. Maximum bottle volume does not indicate rated output at that volume. Operating power and installed power differ, and compressor, chiller and auxiliary loads must be counted separately for total plant power.
Specifications are subject to change. Application suitability, final configuration and performance are confirmed in the approved technical quotation.
Online integration
Blow bottles straight into the filling line.
An additional option for customers who want bottle production linked directly to the filler.
Linked blowing-to-filling arrangement
Bottle discharge connects to a compatible air conveyor or transfer system. Bottle and neck compatibility, controls and accumulation are coordinated with the selected filler.
Match the complete line, including utilities
Blowing output is selected for the actual bottle size, filler demand, operating margin and buffer needs. High-pressure air, air treatment, cooling, power and interlocks are part of integration planning.
Bottle-volume limits vary by model. Maximum volume is not the rated output at that volume.
Project enquiries
Plan your bottle production with us.
Share your bottle sizes, neck finish, required output and operating hours. We select the blowing machine, moulds and auxiliary equipment around your filling line and send a clear technical proposal.